
Inytialgo
Case studies
Real die casting projects: the problem, what changed in the die and the process, and the result on the shop floor.
-
Case study · Simcenter Simsolid
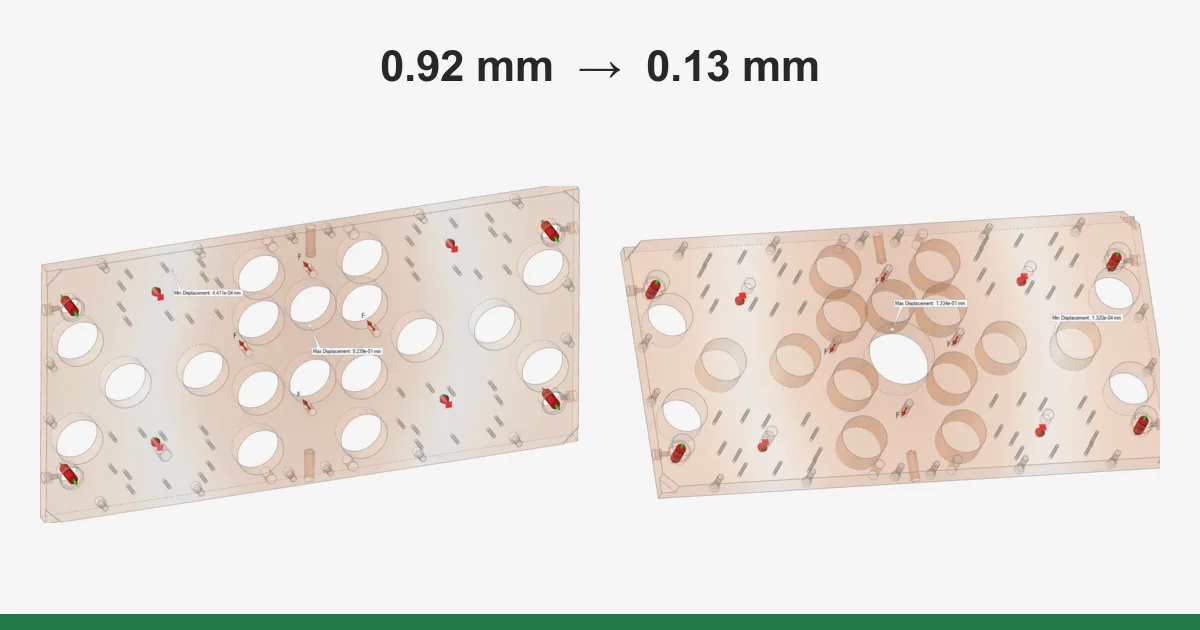
Ejection stiffness in HPDC: from 8 to 3 tonnes of force to eject the same part
A thin-walled part with 0.1 mm flatness: Simcenter Simsolid showed the ejector plate deflecting, and the redesign cut the ejection force from 8 to 3 tonnes.
Read the case
8 → 3 t Force to eject the same part (−62.5%): proof it no longer distorts
-
Case study · Simcenter Inspire Cast
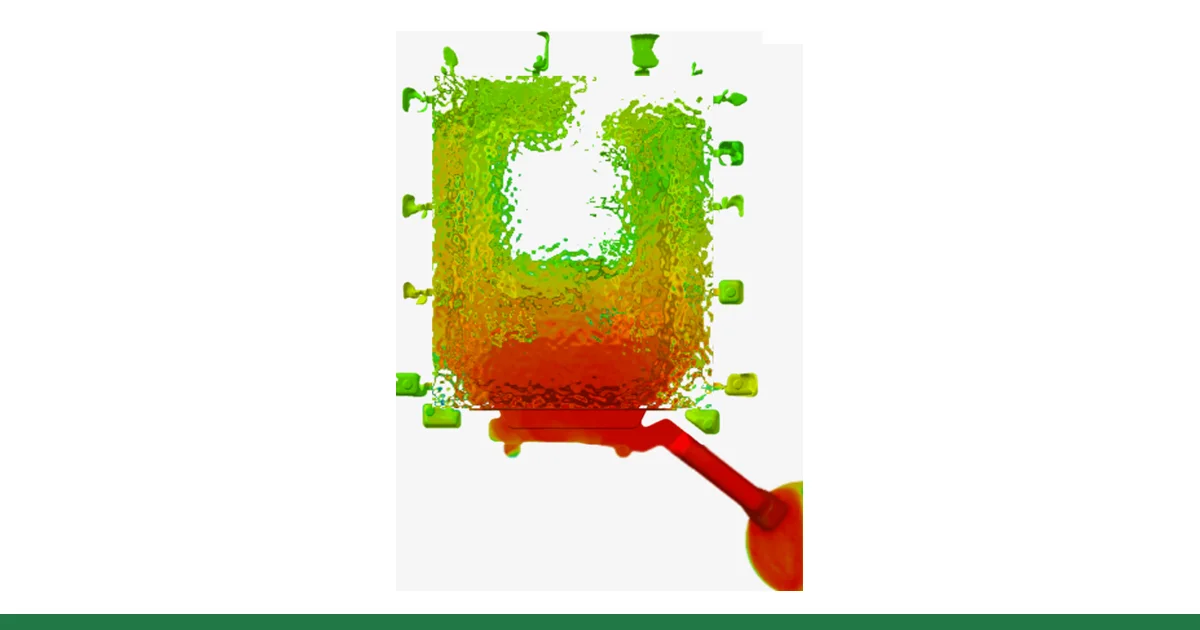
LEAN HPDC: die casting with limited clamping force
A 1,400 cm² part the industry sized for a 900-tonne machine runs on a 580-tonne one: plunger choice, uniform wall, filling in Inspire Cast and thermal overflows.
Read the case
580 t Machine it runs on, where the industry called for 900 t
-
Approach · Vacuum-assisted die casting
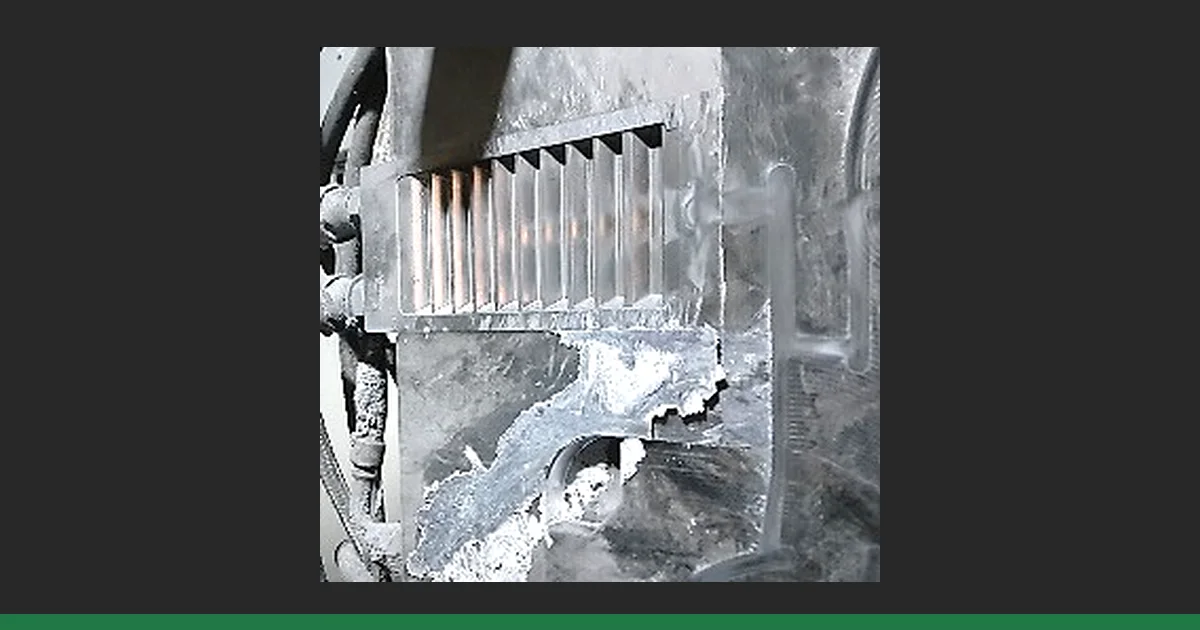
Making vacuum-assisted die casting stick to reduce filling defects
Vacuum with passive chill blocks and one suction point: filling simulation places it, a tight die makes it work and the right device keeps it stable shot to shot.
Read the approach